
Project Description
Lead time 15–20 days
Bevel to ASME B16.25
Quote within 24 hours
PMI 100% of pieces
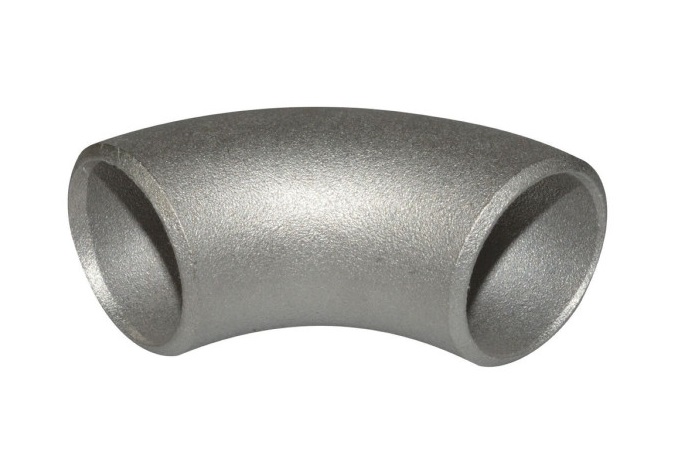
A butt weld elbow changes the direction of a line and is specified by four things, not one: nominal pipe size, schedule, angle and radius. Get any of them wrong and the fitting will not fit — a long radius 90° will not close a gap laid out for a short radius, and a Schedule 10S elbow will not match a Schedule 40S pipe at the bevel. ASME B16.9 fixes the centre-to-end dimensions, the bevel geometry and the wall at each end, so the fitting lines up with the run pipe without a transition piece. We supply 1/2 to 48 inch, 90° and 45°, long and short radius, seamless to 10 inch and welded above, in WP304, WP304L, WP316 and WP316L, with 321, 347, 310S and duplex on request — every piece PMI checked and the bevel machined to B16.25.
Types and size range
Table 1 — What we make, and the range for each
| Type | What it does | Seamless | Welded |
|---|---|---|---|
| 90° long radius (LR) | Standard direction change, radius 1.5 × NPS. The default elbow in most line classes. | 1/2 – 10 in | 1/2 – 48 in |
| 90° short radius (SR) | Radius 1.0 × NPS — tighter, higher pressure drop, used where space is fixed | 1/2 – 10 in | 1/2 – 24 in |
| 45° long radius | Half the direction change, lower pressure loss, often used in pairs | 1/2 – 10 in | 1/2 – 48 in |
| 90° reducing | Changes direction and size in one fitting; both ends stated separately | 1/2 – 10 in | 1/2 – 24 in |
| 180° return | Two 90° in one body; LR or SR | 1/2 – 10 in | 1/2 – 24 in |
| 3D / 5D bend | Longer radius for lower friction loss — pigging, slurry and abrasive service | On request | On request |
Which dimensional standard applies
Table 2 — B16.9, B16.28 and MSS SP-43 are not interchangeable
| Standard | Covers | Use it when |
|---|---|---|
| ASME B16.9 | Wrought butt welding fittings, NPS 1/2 – 48: LR and SR elbows, returns, tees, reducers, caps | The default for any line class written to ASME |
| ASME B16.28 | Short radius elbows and 180° returns only | You are ordering SR elbows and the specification cites it — dimensions match B16.9 for those items |
| MSS SP-43 | Light wall (SCH 5S / 10S) corrosion-resistant fittings | Thin wall stainless where B16.9 wall would be heavier than the pipe |
| MSS SP-75 | High strength wrought fittings, carbon and low alloy | Not stainless — high yield line pipe service |
| EN 10253-4 | European wrought austenitic and duplex fittings | The drawing is European; end-to-end dimensions differ from B16.9 |
B16.28 does cover short radius elbows — that is the one place it is relevant to an elbow order. It does not cover long radius elbows, and it does not cover reducers, which is a mistake that appears on a lot of published data sheets.
Grades
Table 3 — A403 chemistry for the four grades we hold (%)
| Element | WP304 | WP304L | WP316 | WP316L |
|---|---|---|---|---|
| C max | 0.08 | 0.035 | 0.08 | 0.035 |
| Mn max | 2.00 | 2.00 | 2.00 | 2.00 |
| Si max | 1.00 | 1.00 | 1.00 | 1.00 |
| P max | 0.045 | 0.045 | 0.045 | 0.045 |
| S max | 0.030 | 0.030 | 0.030 | 0.030 |
| Cr | 18.0 – 20.0 | 18.0 – 20.0 | 16.0 – 18.0 | 16.0 – 18.0 |
| Ni | 8.0 – 11.0 | 8.0 – 12.0 | 10.0 – 14.0 | 10.0 – 14.0 |
| Mo | — | — | 2.00 – 3.00 | 2.00 – 3.00 |
Table 4 — Mechanical properties and where each grade belongs
| Grade | Tensile min | Yield min | Elongation | Use it when |
|---|---|---|---|---|
| WP304 | 515 MPa | 205 MPa | 28% | General corrosion, no field welding, no chlorides |
| WP304L | 485 MPa | 170 MPa | 28% | The elbow will be welded into the line and cannot be annealed afterwards |
| WP316 | 515 MPa | 205 MPa | 28% | Chloride-bearing and marine service, shop welding with controlled heat input |
| WP316L | 485 MPa | 170 MPa | 28% | Sour, chemical and offshore duty with field welding |
| WP321 / WP347 | 515 MPa | 205 MPa | 28% | Service above 500 °C where stabilisation against sensitisation is needed |
What B16.9 fixes, and what you must state
Table 5 — The parameters that define an elbow order
| Parameter | How it is expressed | What goes wrong if it is omitted |
|---|---|---|
| NPS | Nominal pipe size, e.g. 6 in | Nothing — it is the one thing always quoted |
| Schedule | SCH 10S, 40S, 80S, 160S, XXS | The bevel wall will not match the pipe; welder has to build up or grind down |
| Angle | 90° or 45° | Half the direction change — the line will not close |
| Radius | Long (1.5 × NPS) or short (1.0 × NPS) | Centre-to-end differs by a third; layout is wrong |
| End preparation | Bevel to ASME B16.25, or plain | Plain ends on a butt weld order means the welder preps every joint on site |
| Grade | WP304L, WP316L, etc. | PMI rejects the delivery, or worse, it is installed |
Centre-to-end dimensions are tabulated in ASME B16.9 and we quote against that table — we do not publish our own, because a fitting that is a millimetre out will not close a spool that was fabricated to the standard.
Inspection
Table 6 — Test scope
| Check | Coverage | Method |
|---|---|---|
| Chemical analysis | Every heat | Spectrometer, on the 3.1 certificate |
| PMI | 100% of pieces | XRF — catches 304 substituted for 316L |
| Solution annealing | Every lot | 1040 °C minimum, water quench, recorded |
| Hydrostatic | Every lot, or waived against NDE | Per B16.9 |
| Radiography | On request, welded elbows | Longitudinal seam only |
| Dimension | Sample per lot | Centre-to-end, end OD, wall at both ends, bevel angle, out-of-round |
| Surface | 100% visual | Pickled and passivated; no die marks or laps |
Where stainless elbows are used
Process piping
Every direction change in a chemical or pharmaceutical line. LR is the default; SR only where the layout has no room.
Food and dairy
Hygienic lines with clamp or butt weld joints. The bore must be smooth and the elbow must drain — SR elbows hold product.
Marine and offshore
316L seawater-adjacent systems above the waterline. PMI on every elbow is normally a project hold point.
Pulp and paper
Stock lines where 3D and 5D bends replace standard elbows to avoid fibre build-up at the tighter radius.
Heat exchangers and skids
Compact spools inside packaged equipment, where SR elbows keep the footprint down and pressure drop is not critical.
High temperature
321 or 347 above 500 °C, where the stabilised grades resist sensitisation through repeated thermal cycling.
Frequently asked questions
Long radius or short radius?
Long radius unless there is a reason not to. LR gives roughly half the pressure drop and a gentler flow path. SR is used where the layout is fixed — inside a skid, or replacing an existing fitting without re-fabricating the spool.
What is the actual difference in size?
Centre-to-end is 1.5 × NPS for long radius and 1.0 × NPS for short radius. On a 6 inch elbow that is roughly 229 mm against 152 mm — enough that the two are not interchangeable in a fabricated spool.
Does ASME B16.28 apply to my elbow?
Only if it is a short radius elbow or a 180° return. B16.28 does not cover long radius elbows, and it does not cover reducers at all. If your specification cites B16.28 for a long radius item, the reference is wrong.
Do you supply 3D and 5D bends?
Yes, to order. They are not B16.9 products — the dimensions come from the drawing or from the pipeline specification, so they are quoted individually rather than from a table.
WP304L or WP316L?
304L unless there are chlorides. The L grades are specified because the elbow will be welded into a line that cannot be solution annealed afterwards; without that constraint WP304 is stronger and cheaper.
Can the elbow be supplied with a matched pipe spool?
Yes. We can supply elbow and pipe from the same heat where traceability matters, which removes the mismatch at the bevel that causes most fit-up problems.
What bevel do you machine?
ASME B16.25 as standard: 37½° ± 2½° with a root face of about 1.6 mm. Other preparations on request, including plain ends for clamp fittings.
What is the minimum order and lead time?
20 pieces per size and type. Lead time is 15–20 days; above 24 inch and for 3D bends expect 25–30 days.
Request a quote
Related products
Stainless Butt Weld TeeEqual and reducing, SCH 10S–80S
Stainless Butt Weld CapB16.9, NPS 1/2–24
Socket Weld FittingsASME B16.11 Class 3000 and 6000
O’let FittingsWeldolet, sockolet, MSS SP-97
Threaded FittingsNPT / BSP, Class 3000 and 6000
All pipe fittings — elbows, tees, reducers, caps, olets and flanges · Guide: socket weld vs butt weld, dimensions and weld procedure
Request a quotation
Give us NPS, schedule, angle, radius, grade and quantity. We reply within 24 hours with price, lead time and certificate scope.